Paper Goods Manufacturing in Newcastle-under-Lyme
Paper manufacturing and conversion has deep roots in Staffordshire, historically tied to the packaging demands of the ceramics industry. Pottery is fragile, heavy and was exported worldwide, which created sustained demand for boxes, corrugated cases, protective wraps and printed labels. That legacy shaped a local paper goods sector oriented around protective packaging and print, and much of that orientation survives today.
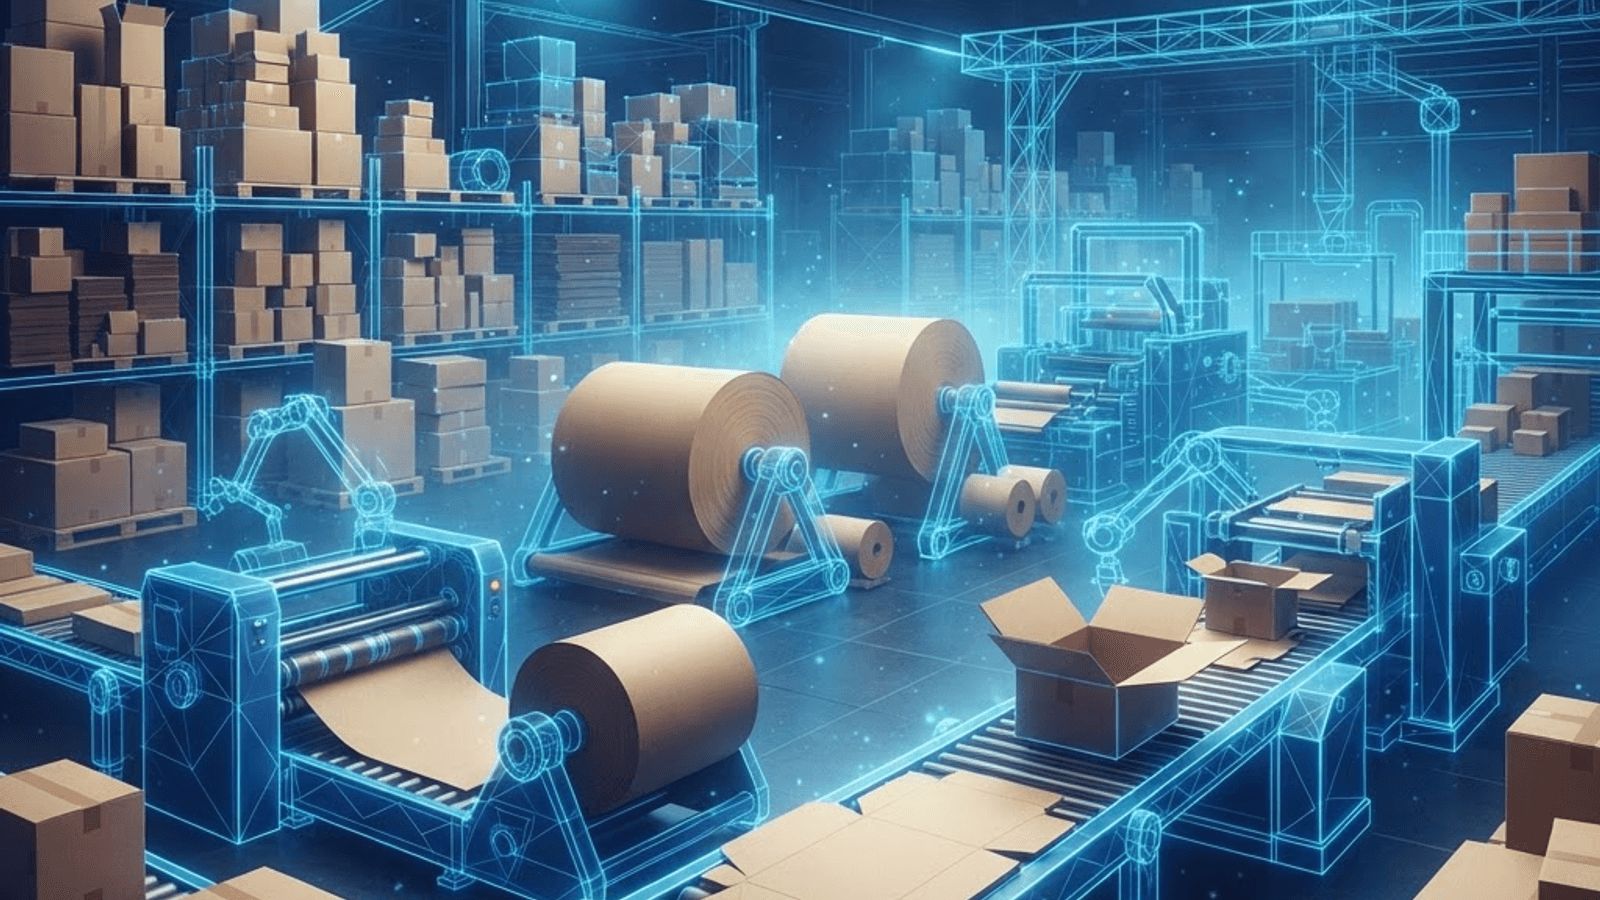
Modern borough manufacturers convert paper and board into corrugated cases, folding cartons, printed labels, bags, tissue and hygiene products, stationery and specialist industrial papers. Very little primary papermaking happens locally; the sector is overwhelmingly about conversion, printing and finishing, which is where the value and the skill increasingly sit.
What the Sector Produces
Corrugated packaging dominates by volume. Single wall, double wall and triple wall board is cut, creased, printed and glued into cases, trays and transit packaging. Die-cut inserts and fitments protect fragile contents, a capability directly inherited from ceramics packing.
Folding cartons in solid board serve retail and food markets, where print quality and shelf presence matter. Label production spans self-adhesive, wet-glue and sleeve formats using flexographic and digital presses. Paper bags and wrapping have seen a resurgence as retailers move away from plastic. Tissue conversion produces hand towels, wipers and hygiene products for commercial washrooms and industrial use.
The Top 10 Paper Goods Manufacturers Serving Newcastle-under-Lyme
1. Lymedale Corrugated. A corrugated case maker producing transit packaging, die-cut boxes and bespoke protective inserts. Its structural design team develops packaging that passes drop and compression testing rather than simply looking correct on a drawing.
2. Chesterton Print & Packaging. Combining litho and digital print with carton conversion, this firm serves food, drink and retail clients needing high-quality printed folding cartons in both short and long runs.
3. North Staffs Label Company. Producing self-adhesive labels on flexographic and digital presses, with variable data, barcoding and specialist substrates for chemical, food and industrial applications.
4. Silverdale Tissue Converting. Manufacturing hand towels, centrefeed rolls, industrial wipers and washroom consumables from parent reels, supplying facilities management and janitorial distributors across the region.
5. Keele Paper Products. A broad converter making envelopes, stationery, notebooks and bespoke paper items for education, corporate and promotional markets.
6. Madeley Protective Packaging. Specialists in moulded pulp, honeycomb board and paper-based void fill, offering plastic-free protective solutions for e-commerce and fragile goods.
7. Borough Bag Manufacturing. Producing paper carrier bags, sacks and food-grade bags with print and handle options, benefiting strongly from retail's shift away from plastic carriers.
8. Trentside Board Solutions. Supplying and converting greyboard, chipboard and rigid board for book covers, presentation boxes and luxury packaging where substance and finish matter.
9. Audley Digital Print. A short-run digital specialist producing personalised packaging, sample packs and low-volume prototypes without origination costs, ideal for brands testing new lines.
10. Newcastle Packaging Design. Focused on structural and graphic packaging design with prototyping capability, working upstream of manufacture to optimise material use and pack performance.
Sustainability: The Sector's Biggest Story
Paper is in an unusual position: it is the material many industries are switching to. The retreat from single-use plastics has driven substantial growth in paper-based packaging, from bags and wraps to moulded pulp protective inserts that replace expanded polystyrene.
That growth brings responsibility. Responsible sourcing through FSC or PEFC certification is standard among credible manufacturers. Recycled fibre content is high across corrugated production, with most cases containing a majority of recovered material. Water-based and vegetable-based inks have largely replaced solvent systems for many applications.
Recyclability of the finished product is the current frontier. Barrier coatings that make paper resistant to grease and moisture can render it difficult to recycle, so manufacturers are investing in dispersion coatings and mono-material constructions that retain performance while remaining recyclable through standard paper streams.
Extended producer responsibility regulations have sharpened commercial focus considerably. Brands now pay fees based on the packaging they place on the market, weighted by recyclability, which creates direct financial incentive to reduce material and design for recovery. Manufacturers who can advise credibly on this are valuable partners rather than mere suppliers.
Print and Finishing Capabilities
Print quality separates commodity packaging from brand packaging. Flexography is efficient for corrugated and label work. Litho lamination delivers photographic quality on corrugated cases. Digital printing eliminates plate costs, making short runs, versioning and personalisation economic.
Finishing adds distinction: spot varnish, matt and gloss lamination, foil blocking, embossing and specialist coatings. For premium products, these processes materially affect perceived value, and access to them locally shortens development cycles considerably.
Choosing a Paper Goods Manufacturer
Start by defining performance requirements honestly. What weight must the pack carry? How will it be stacked, stored and transported? Is moisture exposure likely? Over-specification wastes money, and under-specification causes damaged goods, which costs far more.
Request structural samples before committing to tooling. A physical prototype reveals problems that drawings hide, particularly around assembly time and stacking stability.
Consider total packaging cost, not unit price. A slightly more expensive case that reduces damage rates, packs faster, or fits more units per pallet frequently delivers net savings that dwarf the price difference.
Check lead times and minimum order quantities against your storage capacity. Large minimum runs are only economic if you can store and use the stock before it deteriorates or the design changes.
The Advantage of Local Supply
Packaging is bulky and expensive to transport relative to its value, which gives local manufacturers a genuine structural advantage. Shorter delivery distances reduce cost and carbon, and the ability to collect an urgent order the same day has rescued more than one production schedule. Local manufacturers can also visit a packing line to see how their product performs in practice, which almost always produces improvement ideas.
Final Thoughts
Newcastle-under-Lyme's paper goods manufacturers combine long-established converting skill with genuine innovation in sustainable packaging. As regulation and consumer expectation continue to push brands towards recyclable, fibre-based solutions, the borough's converters are well positioned. Engage them early in product development, be specific about performance needs, and treat packaging as a functional engineering problem rather than an afterthought.
Want your brand featured in front of decision-makers? Publish a guest post or get a link insertion in our guides through AAMAX's guest post and link insertion service.
Helpful Links
 SponsoredAAMAX — Full-Service Digital Agency
Write for Us
Share your expertise with our readers. We welcome guest contributions from industry specialists.
Pitch your idea