Paper Manufacturing in a Changing Market
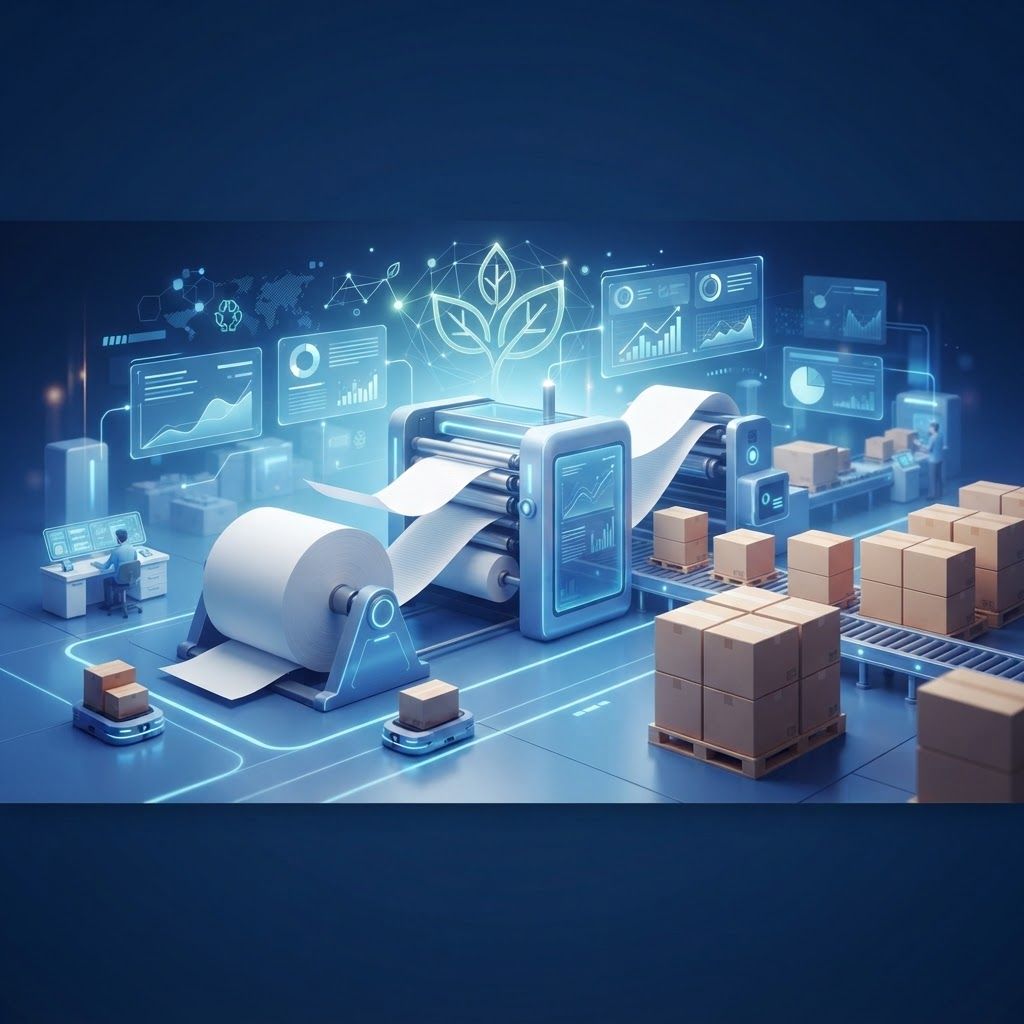
Paper has proved remarkably resilient. Predictions of a paperless world underestimated how deeply paper and board are embedded in packaging, hygiene, labelling and industrial use. In Halton, paper goods manufacturing has evolved accordingly, shifting away from bulk printing volumes towards packaging and converted products where demand continues to grow, driven substantially by online retail and by the substitution of plastic packaging with fibre-based alternatives.
The borough's location supports this trade. Paper and board are bulky and relatively low in value per tonne, so proximity to customers matters enormously. Halton's position between Merseyside and Manchester, with excellent motorway access, allows converters here to serve a dense concentration of manufacturers, distributors and retailers economically.
Understanding Paper Goods Manufacturing
Few companies today make paper from raw fibre in the borough. Most are converters, taking reels or sheets of paper and board and transforming them into finished products through printing, cutting, creasing, folding, gluing and laminating. Corrugated case manufacture, folding carton production, label converting, tissue conversion and specialist industrial paper products all fall within this category.
The Ten Best Paper Goods Manufacturers in Halton
1. Mersey Packaging and Board
Mersey Packaging and Board is the borough's leading corrugated packaging producer, manufacturing transit cases, retail-ready packaging and bespoke protective inserts. The company offers structural design services, producing packaging that protects products through distribution while minimising material use, and provides transit testing to validate designs before full production.
2. Runcorn Carton Company
Runcorn Carton Company specialises in folding cartons for food, pharmaceutical and consumer goods clients. Its capabilities include high-quality lithographic printing, foiling, embossing and window patching, and the firm maintains the hygiene standards required for direct and indirect food contact packaging.
3. Widnes Label Solutions
Widnes Label Solutions produces self-adhesive labels, shrink sleeves and tags for manufacturers across the region. Digital printing capability allows short runs and variable data, supporting product variants, promotional versions and batch-specific information without the cost of conventional plate-based setup.
4. Halton Tissue Converting
Halton Tissue Converting manufactures hygiene paper products including hand towels, wipers and dispenser rolls for commercial and industrial customers. The company works with both virgin and recycled fibre and supplies washroom service providers, facilities managers and industrial buyers throughout the North West.
5. Astmoor Industrial Papers
Astmoor Industrial Papers supplies technical and specialist papers used in manufacturing processes, including interleaving papers, protective wrapping, masking materials and corrosion-inhibiting papers for metal packaging. These unglamorous products solve very specific industrial problems and demand accurate specification.
6. Silver Jubilee Print and Paper
Combining commercial printing with paper converting, Silver Jubilee Print and Paper produces brochures, manuals, stationery and promotional materials alongside bespoke paper products. Its ability to handle both print and finishing in house shortens lead times for clients working to tight deadlines.
7. Halebank Protective Packaging
Halebank Protective Packaging manufactures moulded pulp, honeycomb board and fibre-based cushioning designed to replace expanded polystyrene and plastic void fill. Demand has grown rapidly as brands seek recyclable protective solutions, and the company provides drop testing to prove performance.
8. Ditton Paper Recycling
Ditton Paper Recycling collects, sorts and bales waste paper and board from commercial premises, returning material into the papermaking supply chain. It also offers secure destruction services for confidential documents, with full certification, and provides customers with recycling data for their own reporting.
9. Weaver Valley Bags and Sacks
Weaver Valley Bags and Sacks produces paper bags, multiwall sacks and carrier bags for retail, food service and industrial customers. The shift away from single-use plastic bags has substantially increased demand, and the company offers both plain stock and printed bespoke designs.
10. Norton Priory Stationery Manufacturing
Completing the list, Norton Priory Stationery Manufacturing produces notebooks, pads, files and bespoke printed stationery for corporate and educational clients. Despite widespread digitisation, demand for well-made paper stationery has proved durable, particularly for branded and promotional applications.
Sustainability and Fibre Sourcing
Paper enjoys a genuine environmental advantage in that it is widely recycled and readily biodegradable, but responsible manufacture still demands care. Certified fibre from sustainably managed forests is now the baseline expectation, with chain of custody documentation available on request. Recycled content is used extensively, though fibre length degrades with each cycle, meaning virgin fibre input remains necessary to sustain the system.
Coatings and laminates require particular attention. A board laminated with plastic film may look premium but can be difficult to recycle. Leading converters now offer water-based barrier coatings and recyclable alternatives that maintain grease or moisture resistance without compromising end-of-life recovery.
Water and energy use in converting operations have also fallen significantly through heat recovery, efficient drying and closed-loop water systems in printing operations.
How to Specify Packaging Well
Begin with the distribution journey rather than the product. Understanding how many times a case will be handled, how it will be palletised, what stacking loads it must bear and what climatic conditions it will experience drives correct board grade selection far better than guesswork.
Consider the pack size relationship to pallet dimensions. Small changes in case footprint can dramatically improve pallet utilisation, reducing transport cost and emissions. Engage the converter's structural designers early, as they solve these problems routinely.
Finally, balance print quality against practicality. Elaborate finishes add cost and can complicate recycling, so reserve them for packaging that genuinely functions as a marketing surface.
Conclusion
Paper goods manufacturing in Halton is a practical, quietly innovative sector responding to real shifts in how products are packaged and sold. The companies profiled here combine converting expertise with the design and sustainability knowledge that modern buyers require.
Want your brand featured in front of decision-makers? Publish a guest post or get a link insertion in our guides through AAMAX's guest post and link insertion service.
Helpful Links
 SponsoredAAMAX — Full-Service Digital Agency
Write for Us
Share your expertise with our readers. We welcome guest contributions from industry specialists.
Pitch your idea